A single dust particle on a 9 µm single-mode core can push insertion loss past the limit written into your purchase order, and the connector will still look flawless to the naked eye. Most patch cord disputes between overseas buyers and Asian factories are not about cable jackets or housings — they are about what sat on the end face when the two ferrules mated. This guide covers the zone rules in IEC 61300-3-35, the 2022 revision that changed them, and the inspection records worth demanding.
Why End Face Quality Sets Your Real Link Margin
The arithmetic is unforgiving on single-mode. A 1 µm particle on a 9 µm core blocks roughly one percent of the light path, about 0.05 dB of added loss. Scale that particle to 9 µm and the core is fully occluded. Multimode is more forgiving because a 50 µm core spreads the impact, but the rules still apply — the core zone simply gets a wider radius before zero tolerance starts.
What makes contamination expensive is that it is a chain reaction. Ferrules mate under spring load measured in kilograms, so debris trapped between them is pressed into the glass. Particles and films are usually recoverable with cleaning. A pit or a scratch that reaches the core is not — the glass is physically removed and no solvent brings it back. Debris also deposits on the alignment sleeve inside the adapter, which then contaminates the next cord plugged into that port.
For buyers this is a procurement problem before it is a field problem. Cords shipped without a documented end face check fail on arrival in patterns: one contaminated lot, a supplier that polishes well but packs badly, a run sent in unsealed bags that picks up cardboard fibre in transit. Our fiber optic patch cords ship with per-lot end face and IL/RL data for that reason.
The IEC 61300-3-35 Zone Map in Plain Numbers
The standard defines pass and fail by geometry, not by eye. The ferrule face is divided into four concentric zones measured outward from the centre of the fiber: zone A covers the core, zone B the cladding, zone C the adhesive ring, and zone D the physical contact area out to the ferrule edge. Scratches are linear surface features; defects are particles and pits. Each zone carries its own limit for both.
The table below is the rule set for a single-mode PC connector with return loss of 45 dB or better, which covers most UPC patch cords sold into FTTH and data centre projects.
| Zone | Region | Radius (single-mode) | Radius (multimode) | Scratch limit | Defect limit |
|---|---|---|---|---|---|
| A | Core | 0 – 25 µm | 0 – 65 µm | None of any width | None of any size |
| B | Cladding | 25 – 115 µm | 65 – 115 µm | None wider than 3 µm | Up to 5 between 2 and 5 µm, none larger |
| C | Adhesive | 115 – 135 µm | 115 – 135 µm | No limit | No limit |
| D | Contact | 135 – 250 µm | 135 – 250 µm | No limit | None of 10 µm or larger |
Two details catch buyers out. A defect straddling a zone boundary is graded against the stricter zone, so a particle crossing from zone A into zone B fails the connector even if most of it sits in the permissive zone. And for rectangular ferrules such as MPO/MTP assemblies, the graded requirements apply only to zones A and B of each individual fiber — areas outside the contact zone carry no pass/fail limit, but loose contamination anywhere on the ferrule still has to come off because it migrates.

What the 2022 Revision Actually Changed
The third edition, published in 2022, is the version now referenced in most contracts, and it moved in a direction that helps both sides of a purchase order. Pass and fail criteria for zones C and D were withdrawn. Contamination in the adhesive ring or on the outer contact area does not sit in the light path, so failing a connector for it created rework without protecting performance.
| Item | Edition 2 (2015) | Edition 3 (2022) |
|---|---|---|
| Zone C adhesive verdict | Graded pass/fail | No pass/fail requirement |
| Zone D contact verdict | Defects of 10 µm or larger fail | No pass/fail requirement |
| Zone A multimode scratches | No scratch wider than 3 µm | Up to four scratches of 4 µm or less, none wider than 5 µm |
| Array ferrules | No whole-ferrule step defined | Scan the full ferrule first, then grade each fiber |
| Visual fail vs optical pass | Visual verdict stands | Insertion loss and return loss take precedence |
The most consequential addition for buyers is that optical performance now outranks the microscope. The revision states that a connector failing visual inspection after cleaning but still passing insertion loss and return loss testing may remain in service. If your incoming inspection procedure says any core defect is an automatic reject, you are rejecting cords the standard would accept, and your supplier has grounds to push back on the claim.
The revision also sets tooling expectations. Scanning a full MT ferrule needs a field of view of at least 6.4 × 2.5 mm, wide enough to catch contamination in the 10 µm range anywhere on the array. Grading one fiber’s core and cladding needs a field of view of at least 250 µm, which is what resolves 2 µm defects and 3 µm scratch widths.
APC and UPC Do Not Share an Inspection Setup
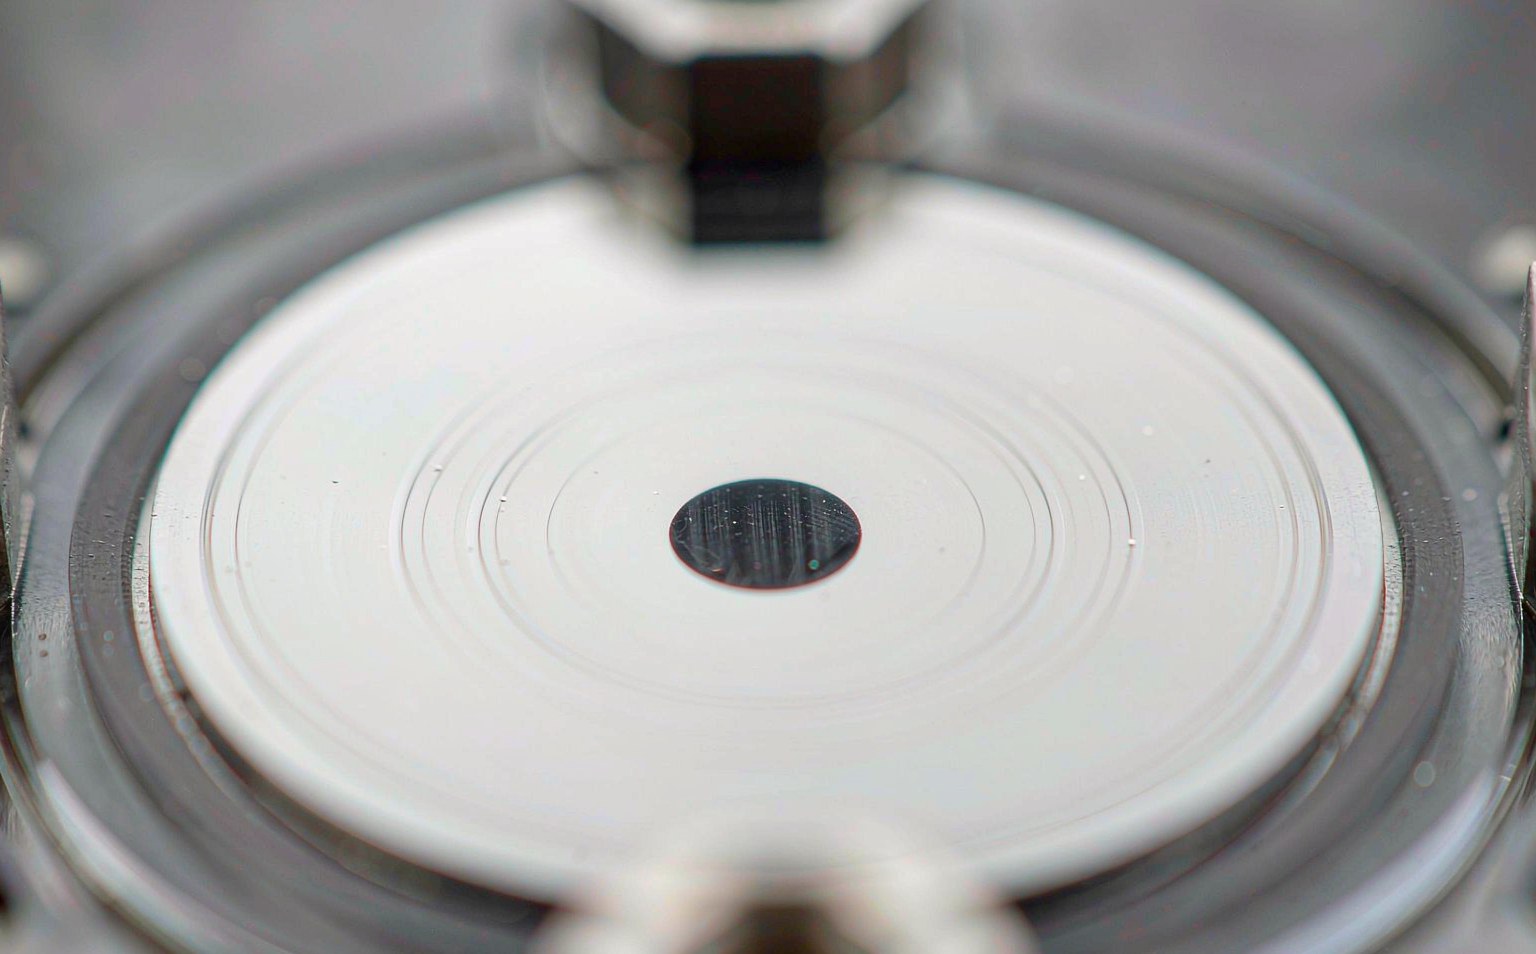
An 8 degree angled ferrule cannot be inspected with a flat probe tip. Push a standard UPC tip onto a green APC connector and the focal plane captures only part of the face, so the core and cladding are out of focus and zoning becomes guesswork. Angled tips compensate for the polish angle and produce a centred image the zone overlay can grade. Ferrule diameter matters too: LC and MU use 1.25 mm tips, while SC, FC and ST use 2.5 mm tips.
Cleaning follows the same logic. The angled surface of an APC ferrule only wipes clean if the tool seats squarely against it; a one-click cleaner that rocks off the angle leaves the core untouched while the operator believes the job is done. Dry cleaning comes first for dust and light film, with a single stroke rather than a back and forth motion that redistributes debris. Wet cleaning with fiber-grade solvent followed immediately by a dry wipe is reserved for silicone oils and heavy film.
The failure modes differ as well. Dust on a flat UPC face creates a microscopic air gap, and return loss collapses because light reflects straight back into the laser. Dust on an APC face tends to offset the angled contact, raising insertion loss through misalignment instead. Connectors that meet ITU-T L.36 end face requirements at the factory can still fail in the field purely on handling.
What to Verify at Goods Receipt
Ask for a distribution, not a typical value. An insertion loss of 0.3 dB typical tells you nothing about the tail of the batch, and the tail is where field failures live. A useful report shows mean, standard deviation and maximum for insertion loss and return loss across the lot, plus the sample size and instrument used. Geometry data from an interferometer matters for high density builds, because radius of curvature, apex offset and fiber height decide whether two ferrules make physical contact across the whole core. Component level characteristics are covered in ITU-T G.671, and the test sequence most carriers cite for connector durability is GR-326.
| Inspection item | Method | Sampling | Value to write into the PO |
|---|---|---|---|
| End face condition | 200× or 400× scope with automatic IEC grading | 100 percent, images retained | Pass on zones A and B, images on request |
| Insertion loss | Light source and power meter, or OTDR | 100 percent single-mode | 0.3 dB typical, 0.5 dB maximum per GR-326 |
| Return loss | Same instrument set, UPC and APC separately | 100 percent | 50 dB minimum UPC, 60 dB minimum APC |
| Ferrule geometry | Interferometer | Per polish lot | Radius 7 – 25 mm, apex offset ≤ 50 µm, fiber height −125 to +125 nm |
| Mating durability | GR-326 cycling | Type test per design | 200 mates, limits held after cycling |
| Environmental category | IEC 61753-1 classification | Type test | Category stated: C, U, O or E |
Spot checks still have a place. Pull five to ten percent of cords on arrival, inspect them with your own scope, and keep the images. It takes minutes per cord and it gives you evidence in the first conversation with a supplier rather than the third. For the arithmetic behind how connector loss accumulates across a span, our walkthrough of insertion loss budget calculation shows where each fraction of a dB comes from, and the reference figures from the Fiber Optic Association and the Fluke Networks fiber inspection resource are worth having on hand when you write the inspection clause.
Procurement Checklist for End Face Inspection
Copy the following into your next purchase order so the acceptance criteria are agreed before goods ship rather than argued about afterwards.
- Name the standard and edition: IEC 61300-3-35:2022, not “IEC compliant.”
- State the polish and return loss class, because the rule set changes with it.
- Require automatic scope grading with saved images, not a manual visual statement.
- Set insertion loss and return loss limits as maximums, not typicals.
- Ask for a per-lot report showing mean, standard deviation and maximum.
- Specify interferometer geometry limits for cords feeding high density panels; the tolerances that matter appear on our LC connector and SC connector pages.
- Reference GR-326 for mating durability and IEC 61753-1 for the environmental category.
- Require sealed, individually capped packaging, since handling after polishing is where most contamination enters.
- Agree the remedy for a failed batch up front, including the adapter sleeves in fiber optic adapters if a shipment contaminates a panel.
- Note that a visual fail with passing IL and RL may be accepted under the 2022 edition, so write the optical limits as the governing criteria.
Send us your test specification and the environment the cords will work in, and we will confirm the polish, the inspection criteria and the report format before the first production run.